-
E-mail
JSGFZL@yeah.net
-
Phone
13962206624
-
Address
No. 112 Xitang Road, Fenghuang Town, Zhangjiagang City
Zhangjiagang Aiguo Biotechnology Co., Ltd
Aiguo Bio Pneumatic Vacuum Feeding Machine: Efficient Material Conveying Solution
Date: 2025-09-05Read: 3
Efficient and clean transportation of materials is crucial in industries such as pharmaceuticals, food, and chemicals. The pneumatic vacuum feeder launched by Zhangjiagang Aiguo Biotechnology has become an ideal choice for many enterprises to optimize production processes and improve production efficiency due to its excellent design and reliable performance.
Innovate working principles to achieve efficient transportation
Zhangjiagang Aiguo Biological Pneumatic Vacuum Feeding Machine cleverly uses compressed air to drive multi-stage jet vacuum pumps or vacuum generators, creating a negative pressure environment within the system. Start the equipment, compressed air flows into the vacuum pump, and a vacuum state is quickly formed in the hopper. The external atmospheric pressure pushes the material into the suction pipe, and under the negative pressure airflow, the material rushes along the conveying pipeline to the hopper for temporary storage. During the process, the filter located between the silo and the vacuum pump accurately intercepts material particles, ensuring that clean air is discharged through the vacuum pump and achieving efficient separation of gas and material. When unloading, the vacuum pump is turned off, the bin door is opened, and the material easily falls to the downstream receiving equipment under the action of gravity, completing one conveying cycle. At the same time, the compressed air stored in the air bag instantly "hits", backwashing the filter and sweeping away the attached particles, preparing for the next suction. This conveying method based on air pressure difference does not require complex mechanical transmission components, and operates stably and efficiently.
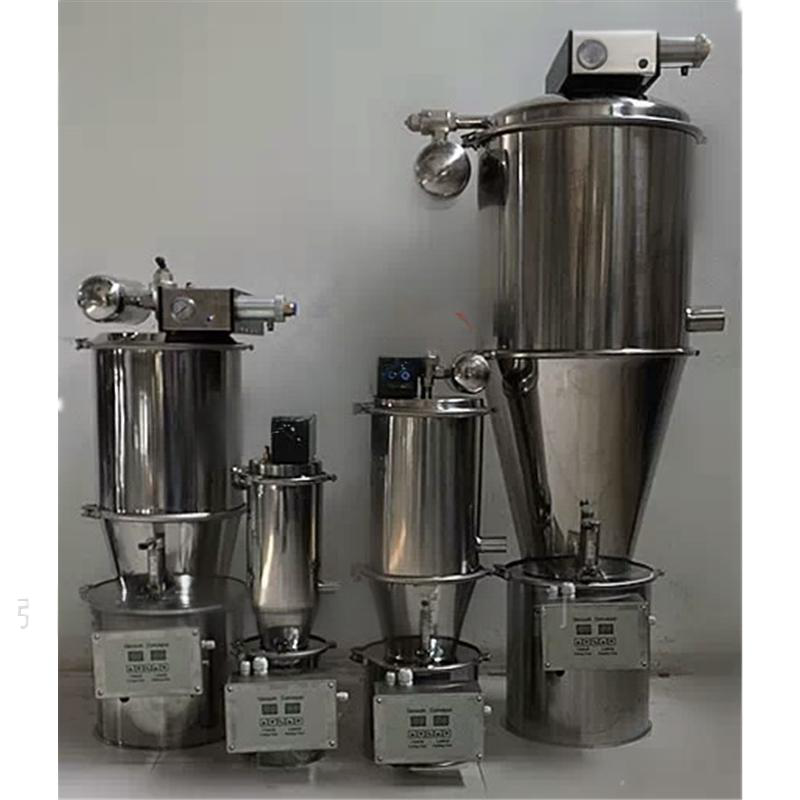
Precise structural design ensures stable operation
1. Power core: Pneumatic vacuum pump and compressed air system
As the power "heart" of the equipment, the pneumatic vacuum pump adopts advanced jet technology and is driven by compressed air without the need for lubricating oil, eliminating faults caused by lubrication problems and significantly reducing maintenance costs. The compressed air system not only provides power for the vacuum pump, but also participates in blowback cleaning. Its pressure and flow rate can be flexibly adjusted according to material characteristics and conveying distance, ensuring stable operation of the equipment under different working conditions.
2. Key defense line: filtration system
The filtration system is the key to ensuring equipment stability and material purity. High quality filters, such as the "Loyal Guardian," accurately intercept material particles with fine filters, preventing them from mixing into the vacuum pump and preventing equipment wear and environmental pollution. The matching anti blowing air path is ingeniously designed, with high-pressure gas backwashing in the opposite direction during unloading, "uprooting" stubborn particles on the filter, maintaining efficient filtration performance, and ensuring smooth and unobstructed suction every time.
3. Material channel: Conveyor components
As a material "transfer station", the silo is equipped with sensitive level gauges or precise delay relays according to production needs to accurately control the suction amount. The suction tube and conveying pipeline are made of high-quality materials, with precision polished inner walls that are as smooth as mirrors. The friction force during material transportation is minimal, avoiding adhesion and blockage. During unloading, the silo door is quickly opened and closed under pneumatic drive to ensure smooth material entry and exit, achieving efficient turnover.
4. Smart Center: Control System
The control system is like the "brain" of a device, finely regulating the suction time, discharge interval, and blowback cycle through knobs, delay relays, or advanced PLC programming. Operators can set parameters with just one click based on material characteristics and production pace, and the equipment can accurately execute instructions to achieve automated and intelligent material conveying.
Excellent performance, meeting diverse needs
1. Efficient and energy-saving, green production
Compared to traditional mechanical conveying equipment, pneumatic vacuum feeders do not require high-power motors and rely solely on compressed air to drive, significantly reducing energy consumption. At the same time, its efficient transportation significantly reduces material turnover time, improves overall production efficiency, and aligns with the company's green and efficient production philosophy.
2. Clean and environmentally friendly, in compliance with GMP standards
The entire conveying process is fully enclosed, with zero contact between the material and the outside air, preventing dust from flying and effectively improving the workshop working environment, ensuring the health of employees. The equipment material and structural design strictly follow GMP standards, are easy to clean, have almost no dead corners, prevent material cross contamination, and meet the production standards of high demand industries such as pharmaceuticals and food.
3. Widely applicable, flexible and versatile
Whether it is fine powder like materials or irregular particle materials, Aiguo Bio Pneumatic Vacuum Feeding Machine can easily handle them. By adjusting equipment parameters and replacing some components, it is possible to adapt to different material characteristics, from lightweight starch to high-density metal powder, from thermosensitive materials to easily hygroscopic materials, all of which can achieve stable and efficient transportation.
4. Stable operation and convenient maintenance
The equipment has few core components, no complex mechanical transmission structure, low vibration and noise during operation, and strong stability. Daily maintenance only requires regular inspections of the compressed air system and filters, with easy replacement of vulnerable parts, significantly reducing the operation and maintenance costs and downtime of the enterprise.
Diversified application scenarios to assist industry upgrading
In the pharmaceutical industry, from raw materials to finished drug production, pneumatic vacuum feeders accurately and cleanly transport materials to ensure drug quality and safety. In food processing, various raw materials such as flour, sugar, and additives are transported to avoid contamination and ensure food safety. In the field of chemical engineering, it is used to transport corrosive, flammable and explosive materials in a fully enclosed manner to eliminate the risk of leakage and ensure production safety. In addition, in industries such as electronics and building materials, efficient and stable material transportation advantages can also be leveraged, injecting strong impetus into the optimization of production processes for enterprises.
Standardize maintenance and prolong equipment lifespan
Regularly inspect compressed air pipelines to ensure no leaks or blockages, and maintain stable pressure within the rated range of the equipment. Clean the filter in a timely manner, replace the damaged filter screen, and ensure the filtration effect. Check the sealing performance of the silo door, replace worn seals in a timely manner to prevent material leakage. Pay attention to the noise and vibration of the equipment during operation, and promptly shut down for troubleshooting in case of abnormalities to ensure long-term stable operation of the equipment.
Zhangjiagang Aiguo Biological Pneumatic Vacuum Feeding Machine stands out in the field of material conveying with innovative technology and excellent performance. Choosing Aiguo Bio Pneumatic Vacuum Feeding Machine lays a solid foundation for improving production efficiency and ensuring product quality for enterprises, helping them stand out in fierce market competition.