-
E-mail
psf@china-jianan.com
-
Phone
15057360160
-
Address
No. 1188 Jiangnan Avenue, Oubei Street, Yongjia County, Wenzhou City, Zhejiang Province (Canaan Technology)
Zhejiang Canaan Technology Co., Ltd
Aseptic packaging isolator constructs a precise barrier for a sterile environment
Date: 2025-10-26Read: 0
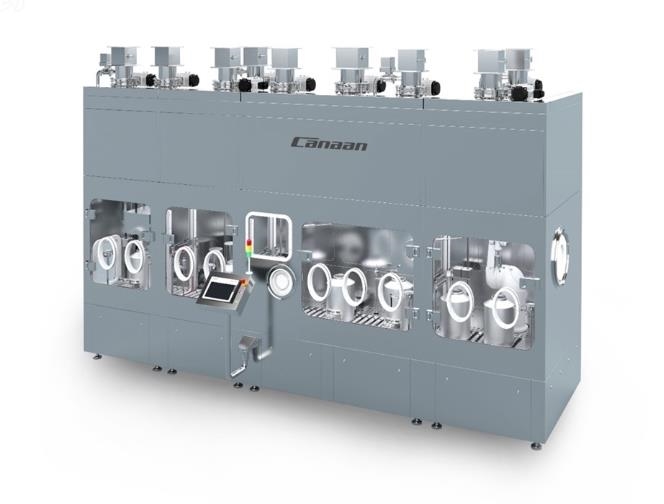
Aseptic packaging isolators are key equipment in the pharmaceutical, biotechnology, and laboratory fieldsIts core function is to build a continuous sterile operating space through physical isolation and dynamic environmental control technology, ensuring that the drug packaging process is free from microbial contamination. Its working principle can be summarized as the collaborative operation of four technical modules: physical barriers, airflow control, sterilization system, and intelligent monitoring.
1. Physical barrier: a rigid structure with absolute isolation
The main body of the sterile packaging isolator is made of stainless steel or high-strength composite materials to construct a closed compartment, and structural gaps are eliminated through seamless welding technology. Operators use rubber gloves integrated into the cabin wall for material handling, and the interface between the gloves and the cabin is designed with double sealing to ensure that no external air infiltrates during operation. The material transfer relies on a fast transfer window or double door interlock system, which maintains a positive pressure inside the cabin during the transfer process to prevent external airflow from backflowing. This physical isolation mechanism separates all operators, environmental microorganisms, and packaging materials, forming a "sterile operation island".
2. Airflow control: dynamic balance of positive pressure environment
The cabin air circulation system achieves three-stage filtration through high-efficiency particulate air (HEPA) filters: the inlet end has a filtration efficiency of 99.97% (0.3 μ m particles), the cabin maintains a positive pressure of 20-50Pa, and the exhaust end is equipped with an H14 level filter to ensure that the exhaust gas is sterile. The airflow organization adopts a unidirectional laminar design, where air is uniformly sent down from the top and discharged from the bottom after passing through the operating area, forming a vortex free airflow barrier. The temperature and humidity are precisely adjusted through an independent control system to prevent the growth of microorganisms in condensed water.
3. Sterilization system: three-dimensional disinfection and sterilization of hydrogen peroxide
The integrated vaporized hydrogen peroxide (VHP) sterilization module atomizes 35% hydrogen peroxide solution into micrometer sized particles through a nozzle, evenly covering all surfaces inside the cabin. The sterilization cycle is divided into four stages: pre cooling, atomization, holding, and residual removal. All microorganisms, including spores, can be killed within 60 minutes. After sterilization, the concentration of hydrogen peroxide is reduced to below 0.1ppm through a catalytic decomposition device to ensure material safety. Some models are equipped with UV-C ultraviolet auxiliary disinfection system to perform secondary disinfection and sterilization on the operating table.
4. Intelligent monitoring: real-time feedback quality control
The cabin integrates a particle counter (monitoring particles ≥ 0.5 μ m), a planktonic bacteria sampler, and temperature and humidity sensors, and the data is transmitted in real-time to the PLC control system. When the pressure difference fluctuates beyond ± 5Pa or the particle count exceeds the standard, the system automatically triggers an alarm and suspends operation. The glove integrity testing adopts pressure attenuation method, and leakage testing is conducted monthly. All environmental parameters and operation records are automatically stored on the local server, in compliance with GMP data traceability requirements.
This technology system makes sterile packaging isolators a standard equipment for high-risk drug production, with a sterile assurance level 1000 times higher than traditional cleanrooms, while reducing operating costs by 30%. With the strengthened requirements of EU GMP Appendix 1 for pollution control strategies, sterile packaging isolator technology is evolving towards modularity and intelligence, providing more reliable sterile operation solutions for the biopharmaceutical industry.