-
E-mail
GXM7788@126.COM
-
Phone
13958337766
-
Address
Xinqiao, Xiangshan County, Ningbo City, Zhejiang Province
Ningbo Xuming Pharmaceutical Equipment Co., Ltd
Ningbo Xuming Pharmaceutical Dual Filter: Pharmaceutical grade Precision Filtration Solution
Date: 2025-08-22Read: 7
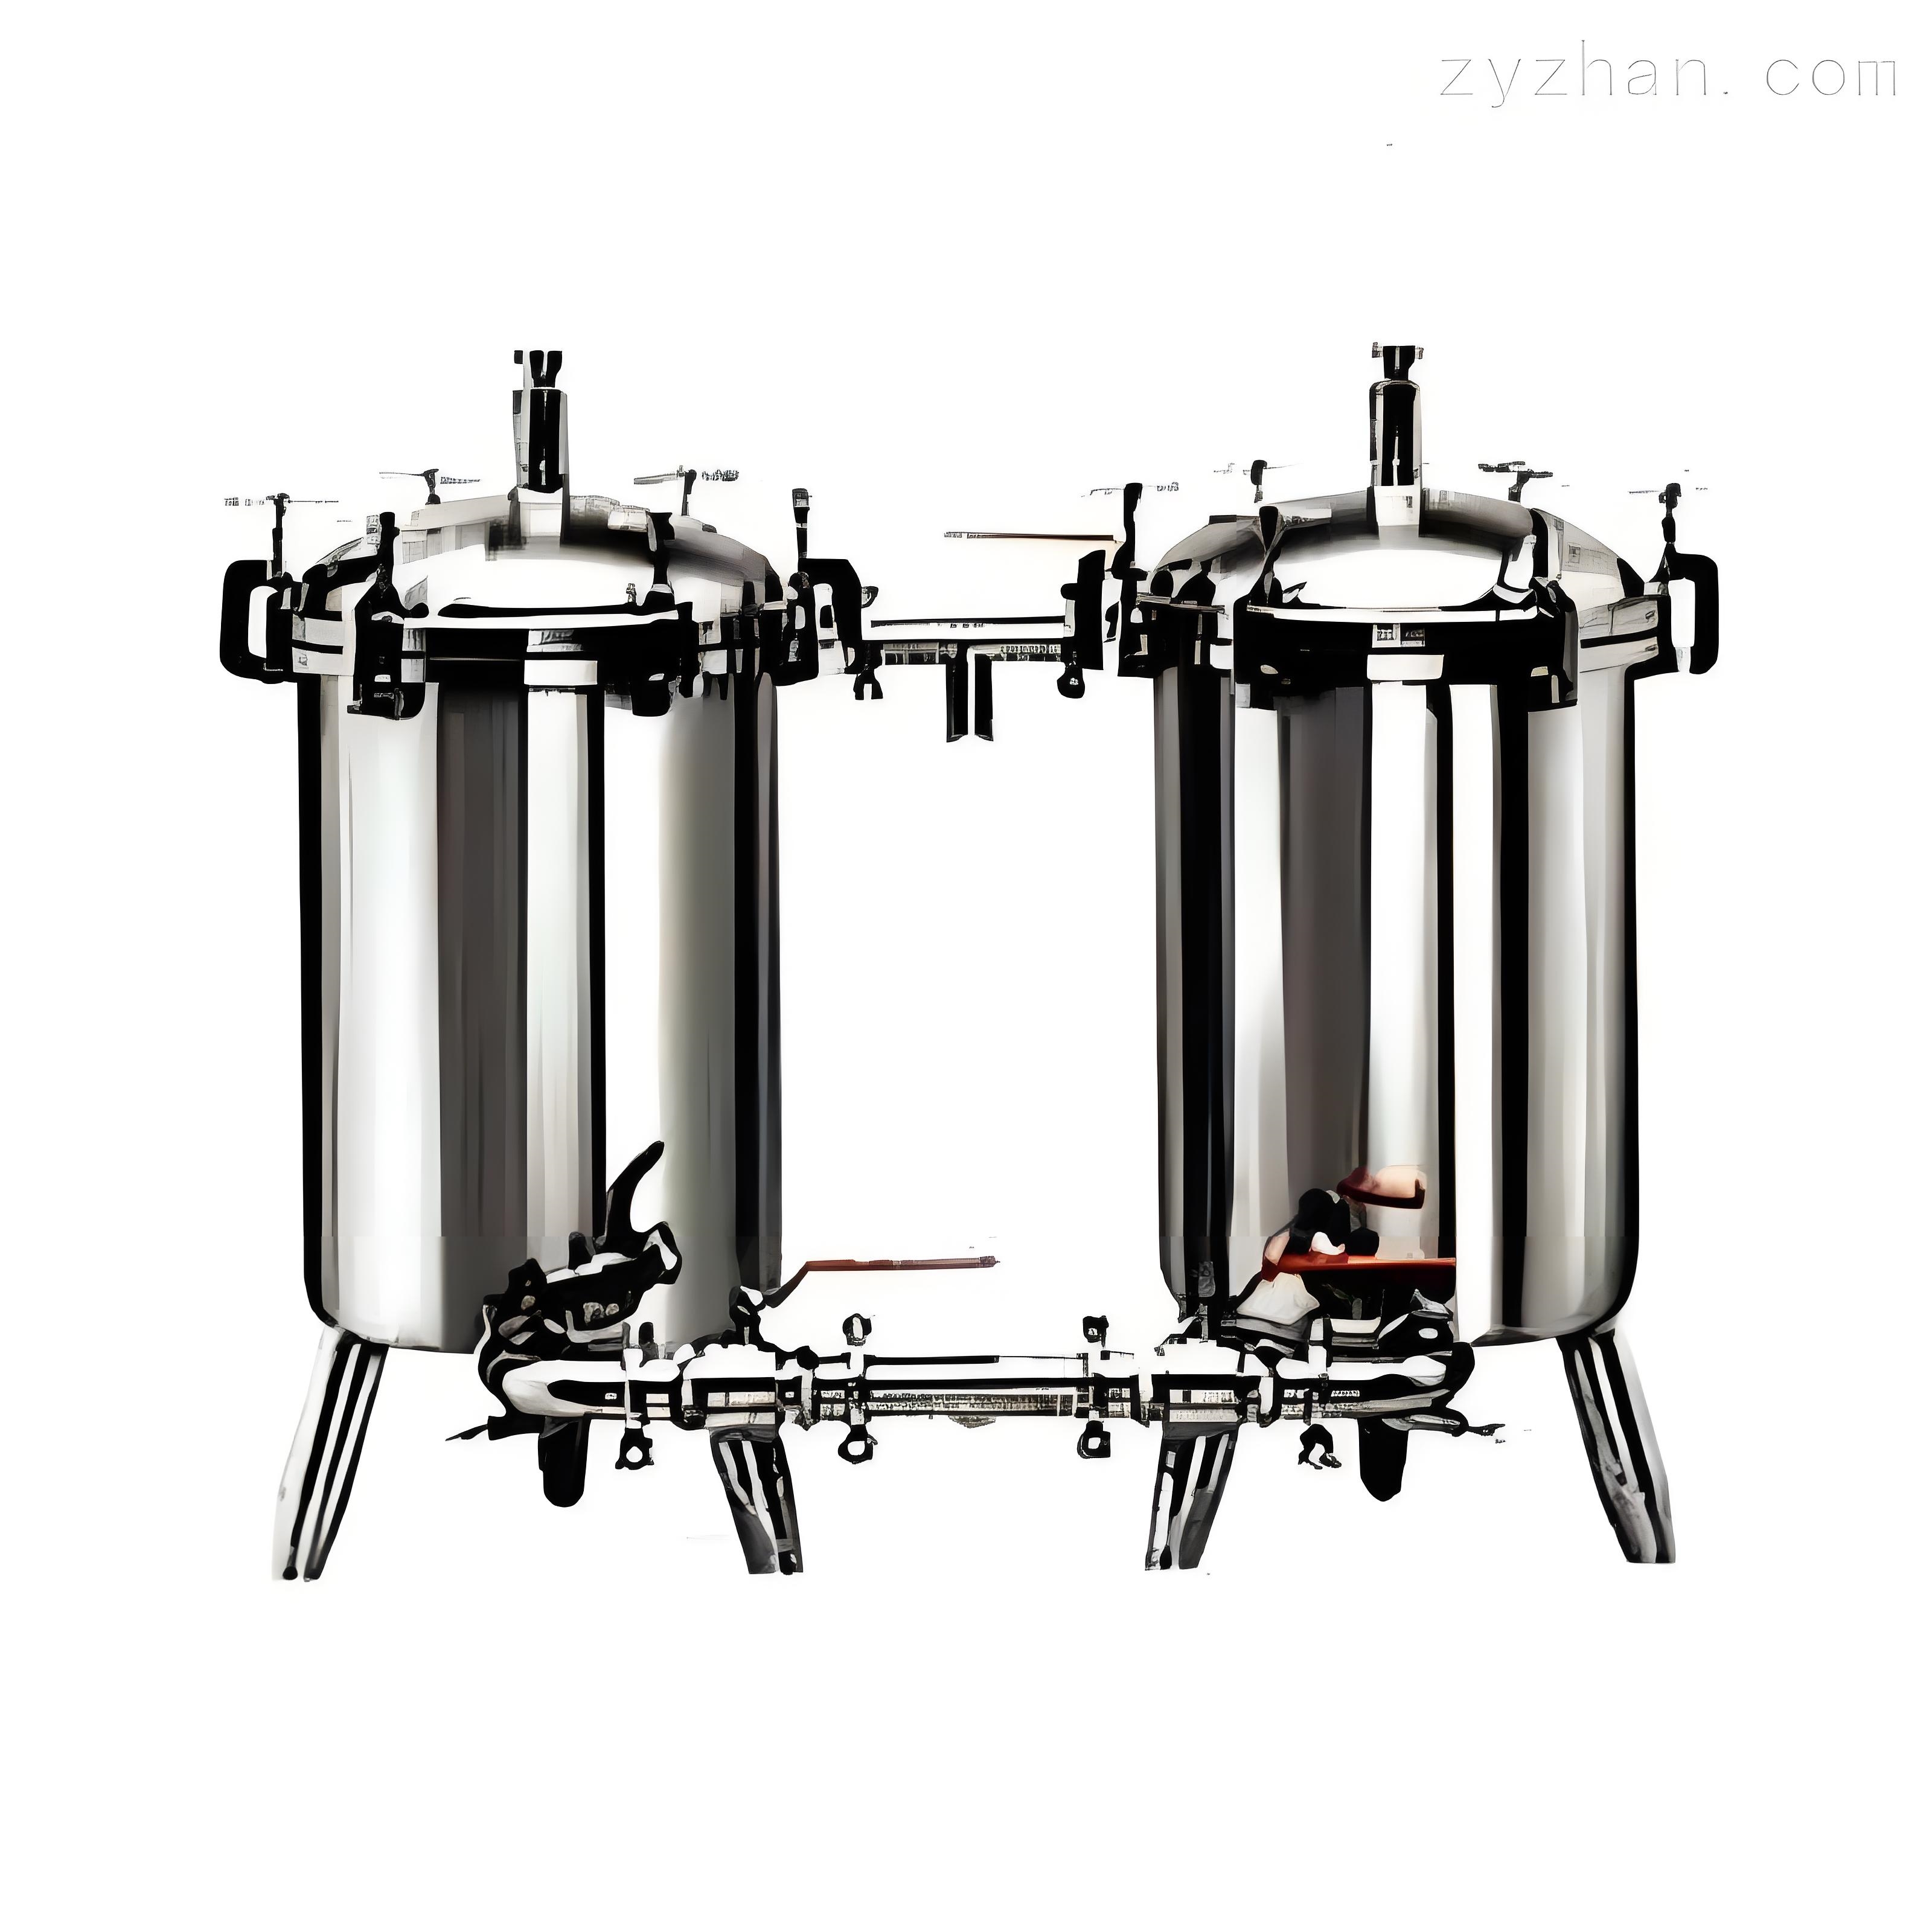
Ningbo Xuming Pharmaceutical's dual filter is designed specifically for the high standard production needs of the pharmaceutical industry. Its core advantage lies in the combination of uninterrupted filtration and high-precision control. The equipment adopts a dual tank parallel structure, which achieves synchronous production and cleaning through intelligent switching valves, ensuring zero interruption in the liquid filtration process and meeting the continuous production requirements of GMP workshops.
Core structural characteristics
Modular design: The main body is made of 316L stainless steel material, and the surface of the filter tank is mirror polished (roughness Ra ≤ 0.28 μ m). It is equipped with a quick opening clamp structure, which shortens the replacement time of the filter element to within 5 minutes and significantly improves maintenance efficiency.
Precision filtration system: supports dual-mode switching between filter bags (precision 1-400 mesh) and filter cartridges (0.1-10 μ m), and a specially designed side leakage detection device can intercept 99.9% of particle offset, ensuring stable filtration accuracy.
• Automation control: Integrated PLC control system, real-time monitoring of pressure difference and flow data. When the pressure difference exceeds 0.1MPa, the backwash program is automatically triggered, reducing the water consumption of sewage by 60% compared to traditional equipment.
Advantages of pharmaceutical applications
Aseptic assurance: In the production of biological agents such as insulin and vaccines, the equipment is validated through a 0.22 μ m sterilization grade filter membrane, and the microbial retention rate can reach Log6 standard, meeting the requirements of aseptic inspection.
Wide compatibility: Suitable for high viscosity drugs (such as syrup, oral liquid) and corrosive solvents (such as ethanol extract), acid and alkali resistant pH range 2-12, material certified by FDA.
Energy saving and consumption reducing: The dual effect heat exchange design achieves a heat recovery rate of 75%, and with the cooperation of variable frequency pump units, the comprehensive energy consumption is reduced by 30%.