-
E-mail
hpewater@126.com
-
Phone
13504432851
-
Address
13-101, No.1019 Fengshuo Road, Qikai District, Changchun City
Product Categories
- water purification equipment
- Nanofiltration membrane concentration equipment
- Nanofiltration membrane purification equipment
- Laboratory membrane separation device
- Bag filter equipment
- EDI Ultra Pure Water Equipment
- Membrane separation equipment
- Microfiltration membrane filtration equipment
- Bag Filter
- Activated carbon filter
- Multi media filter
Jilin Haipu Technology Development Co., Ltd


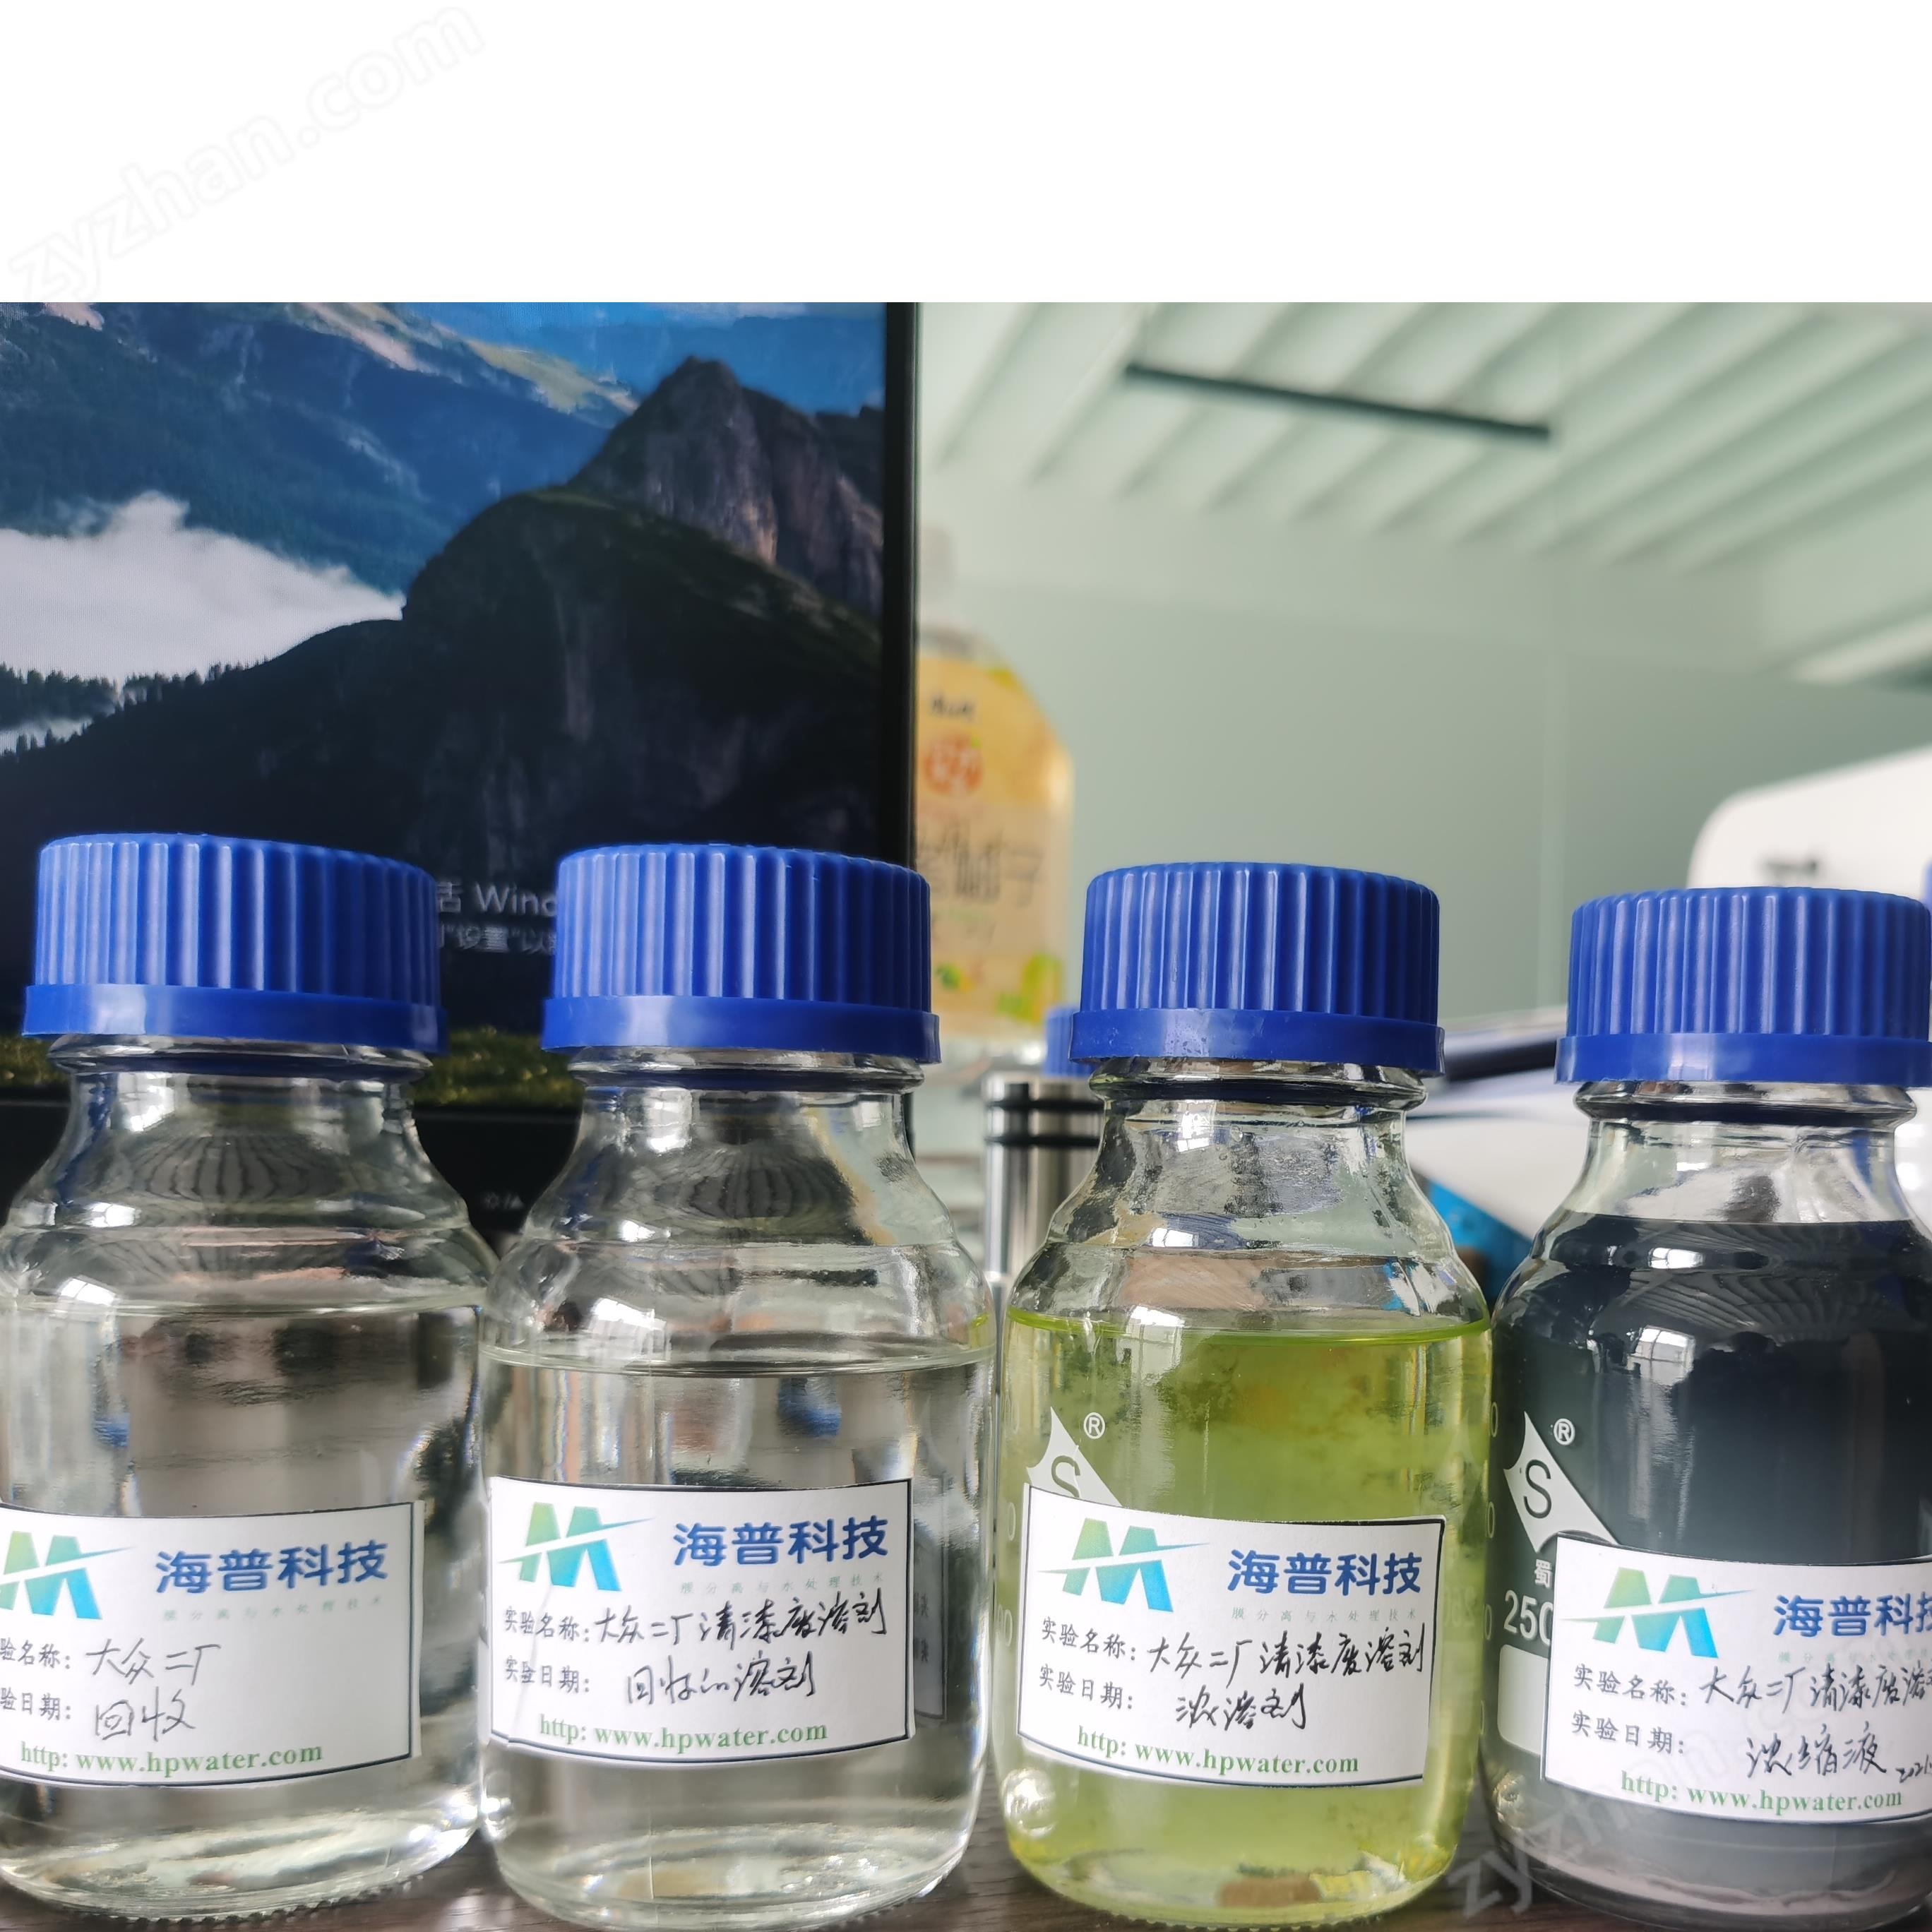


Solvent purification and reuse equipment
NegotiableUpdate on 01/05
- Model
- Nature of the Manufacturer
- Producers
- Product Category
- Place of Origin
Overview
The solvent purification and recovery equipment uses solvent resistant film, and the system is designed and manufactured according to explosion-proof standards. Can be used for the separation, purification, and purification of solvent system materials, working at room temperature, safe and reliable, and highly efficient.. They have excellent stability in non-aqueous solvents and can provide users with extraordinary product value in numerous applications in the chemical industry. The benefits of OSN include lower product costs, less energy consumption, and higher yields for separation at mild ambient temperatures.
Product Details
Solvent purification and reuse equipment
Solvent recovery system
The amount of cleaning solvent generated is enormous
➢Aromatic hydrocarbons, esters and other solvents
➢high-throughput
➢Replace distillation recovery process
➢Reduce operating costs
➢energy conservation and emission reduction
Concentrate raw materials
➢Target product at concentrated concentration50000 ppmThe permeate is concentrateddegree40 ppm
➢High interception rate, high throughput(>50 LMH)
➢Permeation solution is recycled as an extraction solvent
➢Low temperature operation, shorten operation time, avoid thermal concentration damageAPI
➢Energy consumption reduction exceeds70%
➢VOCSignificant reduction in emissions
Natural extract concentration
➢Green and gentle, with improved quality
➢Ethyl acetate solution, thermosensitive natural plant extract
➢Mild concentration, operated at room temperature to ensure that the product does not deteriorate
➢30 barOperating pressure, up to50 LMHFlux, highly concentrated
▪Concentrate effective substances▪Impurity removal
Electronic grade solvent purification
➢Physical filtering
➢High metal impurity extraction rate
➢Low energy consumption and low emissions
➢Modular combination, green manufacturing
Separation and recovery of homogeneous catalysts
➢Accumulation of heavy metals in organic phase
➢Organic solution containing chromium acetate, with a chromium concentration of approximately8000 ppm
➢rejection rate>99%
➢PuraMem FluxMembrane, effective membrane area32m2, SingleHourly processing capacity of support membrane120L-150L
➢Reduce waste disposal volume and lower processing costs
➢Recovery of homogeneous catalysts of precious metals
➢The catalyst remains active and the reaction conversion rate remains high
➢Low heavy metal content in the product
➢Catalyst recycling
➢Reduce operating costs
Separation and recovery of homogeneous catalysts
We offer▪Collaborative development process▪Provide multiple grades of solvent resistant nanofiltration membranes▪Overall process solution▪Open win-win cooperation model

Solvent purification and reuse equipment
electronicOrganic solvent nanofiltration: a new frontier in the field of molecular separationIn the late 20th century, it was already possible to achieve molecular level separation using separation membranes in aqueous solutions, followed by reverse osmosisPermeation and nanofiltration achieve the separation of ions and other molecules. Until recently, both separation technologies were almost exclusively used for wastewater treatmentProcessing, desalination, and food and beverage industries.In the past decade, membrane separation (organic solvent nanofiltration) of molecules dissolved in organic liquids has become a scientific research in membrane separationThe new field of research has broad application prospects in the chemical related industry.This reflects the great benefits it contains. Why? Common purification processes such as distillation, extraction, chromatographic analysis, adsorptionCrystallization is either an energy intensive process, a raw material intensive process, or there may be stability issues. People generally believe that,“……The separation process accounts for a significant portion of industrial capital and operating costs40-70%……”.. We can perform a simple calculation, inConcentrate solutes in specific solvents10 times,useUnited NationsThe energy consumed by the process is less than that of thermal separation technology(Like distillation)of10%.Obviously,United NationsIt can significantly reduce costs.Grade solvent purification schemeElectronic grade solvent purification schemeElectronic grade solvent purification schemeElectronic grade solvent purification schemeElectronic grade solvent purification schemeElectronic grade solvent purification scheme
natural extract
Extract concentration
Concentrate raw materialsConcentrate raw materials
solventsolvent recoveryrecycle
Similar Product Recommend


